1. Get the accounting right: 95% and 90% are not a 5% gap
The light path of a finished luminaire is “source → optical part → space”. Source efficiency keeps improving, but the optical part is always a loss term: every interface reflects some light, and scattering sends part of it to the ceiling rather than the work plane.
The problem is that many spec sheets say only one thing: “transmittance ≥ 90%”. That sentence has three holes:
- Transmittance is a range, not a metric. Extrusion formulation can push transmittance from nearly opaque all the way to 97%, and it never moves alone: it trades off against haze. Push transmittance up and haze usually drops, which is when individual LEDs start showing in the near field.
- Acceptance is judged on the whole luminaire, not the sheet data. LED pitch, mixing distance, and panel height together decide whether you see “grain”. The same sheet looks like hotspots in a thin panel light with only 20 mm of mixing distance, but clean in a bracket light with enough mixing space.
- The time dimension is missing. 92% at shipment and 84% after two years; that 8% drop is what drives the complaints.
The question worth asking is “given the mixing distance and uniformity requirement, where does the optimal transmittance–haze combination land?” That answer comes from optical testing and sampling, not from a brochure number.
2. Three typical failure scenes, where the root cause is often not the source
1. Graininess and hotspots: not enough haze, or the wrong approach.
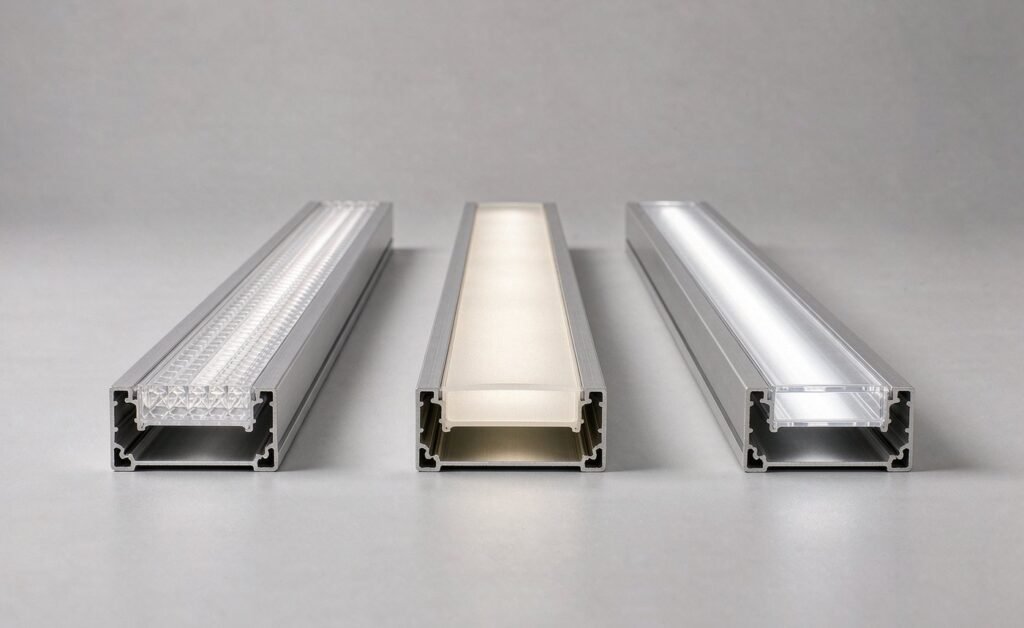
The most common wrong fix is “thicken the diffuser to improve hiding”. You hide the grain, and whole-luminaire efficiency drops 8%, so the client’s lm/W misses the delivery target. The same trade-off sits behind choosing between clear and frosted diffusers. A better split: let the structure do the beam shaping and the diffusion do the uniformity. Use a prism or micro-structure layer where you need control (prism covers commonly span 23–195 mm in width), and a thin, efficient diffusion layer where you need soft light. Thickening alone buys hiding with output.
2. Yellowing and two-year dimming: choose material from the use environment.
PMMA and PC are the two mainstream diffuser materials, with a clear trade-off:
| PMMA | PC | |
|---|---|---|
| Initial transmittance | Higher | Slightly lower |
| Weathering / anti-yellowing | Clearly better | Depends on UV-resistant formula |
| Toughness / impact | Brittle, sensitive to stress cracking | Good, suits snap-fit stressed structures |
| Flame rating | Mostly HB | Easier to reach V-2 / V-0 |
Simplified rule: for indoor, dry environments where output efficiency and long-term colour stability come first, such as linear and panel lights, prefer PMMA; where impact, drop tests or flame ratings are required, use PC or a flame-retardant formula. High power density plus long-term heat plus UV is the fastest route to LED diffuser yellowing; there, the weathering grade of the diffuser and formulation must be written into the spec.
3. Seam shadows and field rework: the ignored dimensional consistency.
Linear lights often run ten-plus meters continuously. Any straightness deviation, twist, or wall-thickness variation becomes a visible misaligned dark seam once installed. Extruded profile weight runs from 10 g/m to 2000 g/m, and weight sets material cost as well as rigidity and snap-fit retention. Compare suppliers on price alone and skip weight tolerance, and the difference shows up as field labor.
3. Beam angle follows the layout parameters, not a sample you liked
Common lens angles are discrete steps like 35°, 45°, 60°, 85°, 95°, 100°, 105°. At the same LED pitch, moving from 60° to 90° may barely change average illuminance, while uniformity (min / average ratio) and glare control differ markedly: narrow angles suit accent lighting in high spaces, wide angles suit an even spread across low spaces, and batwing distribution is often used in linear lights to suppress high-angle glare.
The order that works: derive the required photometry from mounting height, pitch ratio and target UGR first, then choose the angle. Picking a sample and testing it backwards tends to produce something that passes rather than something that fits.
4. An RFQ checklist for practitioners
Write these seven items clearly before sending an inquiry, and you save at least two rounds of back-and-forth:
- Profile cross-section drawing (with tolerances), marking functional faces: which face must be free of flow marks, which is the mating face;
- Target transmittance range, and acceptable hiding standard (whether LED outline is allowed);
- Use environment: long-term operating temperature, outdoor or not, UV or chemical contact;
- Flame rating and compliance (UL94, RoHS, REACH, etc.);
- Material preference (PC / PMMA / FR formula), and whether supplier substitution is acceptable;
- Target weight range, not just price per meter;
- Sampling requirement: sample length, whether full-luminaire photometry validation is needed.
Optical parts are a small share of unit cost and a large share of acceptance risk. Send the constraint set instead of a single transmittance number, and the quotes come back describing your luminaire rather than the supplier’s catalogue.